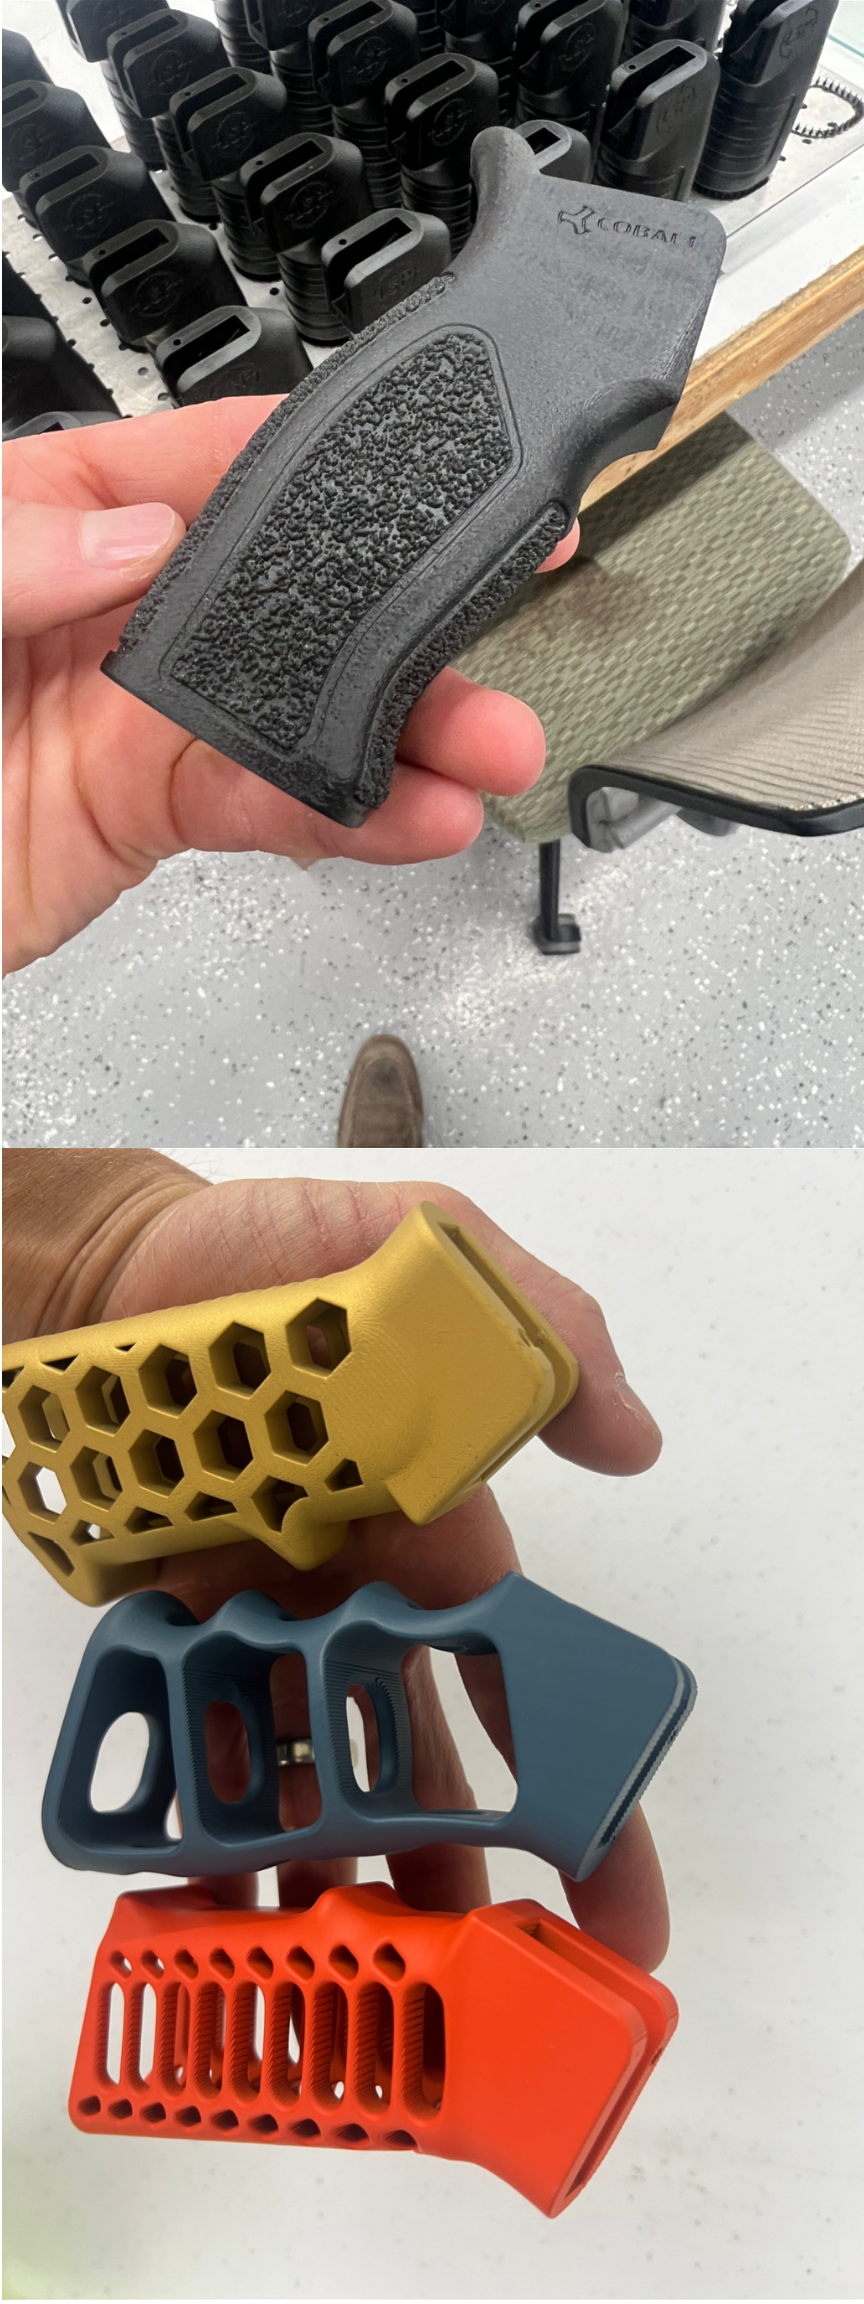
The texture on this grip was never knurled, molded, or wrapped. It was printed, down to the last cell, and that difference changes how a firearms company gets to think about its products.
The problem
On a molded grip, the texture lives in the steel. Want a more aggressive pattern, a different cell size, a new palm swell? That is a tool regrind or a new mold, weeks of lead time, and enough cost that texture experiments have to be rationed. For a premium firearms brand like Cobalt Kinetics, where ergonomics and appearance are the product, rationed iteration is a real constraint.
There is also the bar the industry itself sets: dimensional consistency, durability, a finish worthy of the platform, and accountability on every lot.
What we did
We print the grips 32 to a build in Price, Utah, with the texture carried entirely in the geometry: the honeycomb pattern, the palm swell, the surface feel, all of it in the file. When the design team wants a new pattern, the next build simply prints it. No regrind, no new tool, no six-week wait between idea and part in hand.
After printing, the grips are finished in Cerakote. The printed surface takes the coating cleanly, and the colored set in the photo is the same part proving out finish options: gold honeycomb, slate blue, competition orange. New texture to coated part in a handful of builds is a loop a mold has never offered anyone.
The numbers
- 32 grips per build
- 0 tooling, 0 regrinds across every texture revision
- Texture or ergonomic change: one file revision
- Finish variants proved on real parts, not renderings
Texture is geometry now
The broader point reaches well past firearms. Any product that sells partly on feel, such as hand tools, sporting goods, medical handles, or consumer hardware, has been designing texture around what a mold can eject. Printed production removes that ceiling: the surface your industrial designer actually wants is just more geometry, at no additional cost per part. We covered the design mindset in Quit Drawing Molded Parts.
Get a number for your part
Upload a CAD file for an instant estimate, ask about coating and finishing options, or talk to a real person about a production program.